Built for machine shops and automation
NEMA 12 Enclosures for CNC Machining and Industrial Automation
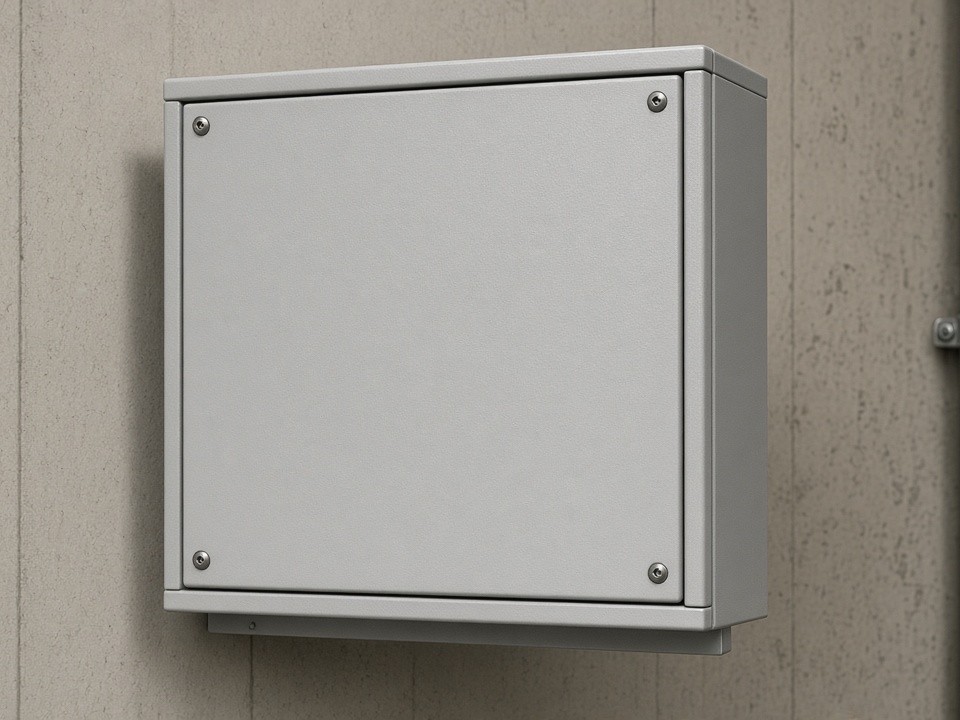
Enclosuremfg produces NEMA 12 rated cabinets to help keep oil mist, coolant spray, and fine metallic dust outside your control compartment. No knockouts means fewer paths for drip oil to enter during long production runs.
Prototype batches from 10 units to recurring annual releases of several hundred.
Protection in cutting-fluid environments
Designed to keep shop-floor contaminants out
NEMA 12 defines protection against falling dirt, circulating dust, and non-corrosive liquids. Around lathes, mills, and grinding stations, that means addressing coolant spray, airborne oil particles, and suspended droplets that can reach control equipment.
The no-knockout design removes common leak paths. Enclosures are built with no open holes except those specified on the approved drawing—helping prevent drip oil from entering during extended production runs.
Coolant spray
Protection for equipment near circulating, non-corrosive liquids.
Oil mist
Built for machining areas where airborne oil particles are common.
Fine dust
Helps keep falling dirt and circulating dust outside the compartment.
Manufacturing process
Sealed construction, made in-house
A coordinated production flow controls panel quality, seam integrity, hardware installation, finish, and final verification.
01 / Cut and form
Laser cutting and precision forming
Panels start on 12 kW and 6 kW fiber lasers, producing clean edges without burrs that could compromise gaskets. Multi-axis CNC press brakes form consistent radii and return flanges for continuous metal-to-metal contact lines—without later patching or secondary sealing plates.
02 / Weld and install
In-house seams and captive hardware
Structural seams receive low-distortion laser welding or full-penetration MIG welding, selected according to load requirements. Automated clinching equipment installs captive PEM fasteners and blind threaded inserts instead of field drilling.
03 / Finish
Large-format powder coating
Weldments move directly to the 2500 × 6000 mm automated powder line for pretreatment, electrostatic application, and thermal cure. The finish provides chemical resistance against cutting fluids, with matte or textured appearance options suited to factory environments.
04 / Verify
Final checks before dispatch
Six dedicated QA personnel perform dimensional checks after forming, weld integrity inspection, and gasket compression testing. First-article reports and material certificates accompany every production batch.
Typical projects
Made for real production environments
From prototype quantities to repeat production, enclosures can be specified around equipment dimensions and fluid exposure.
-
Five-axis machining centers
Operator consoles requiring 4–6 meter frames.
-
Battery module assembly
Electrical cabinets exposed to glycol-based coolants.
-
Transfer lines
Standalone junction boxes mounted where oil mist is constant.
Project planning
What to include with your inquiry
Submit drawings or a basic dimensional sketch along with expected fluid exposure details. Engineering will return a DFM review and firm quotation within two working days.
Useful project details
- Drawings or overall dimensions
- Coolant, oil mist, or other fluid exposure
- Expected batch size and release schedule
Request pricing and lead times
Share your enclosure requirements with our team to begin a DFM review.
Email: info@enclosuremfg.com
Address: Building 4, Kuiqing Road, Qingxi Town, Dongguan City, Guangdong Province